
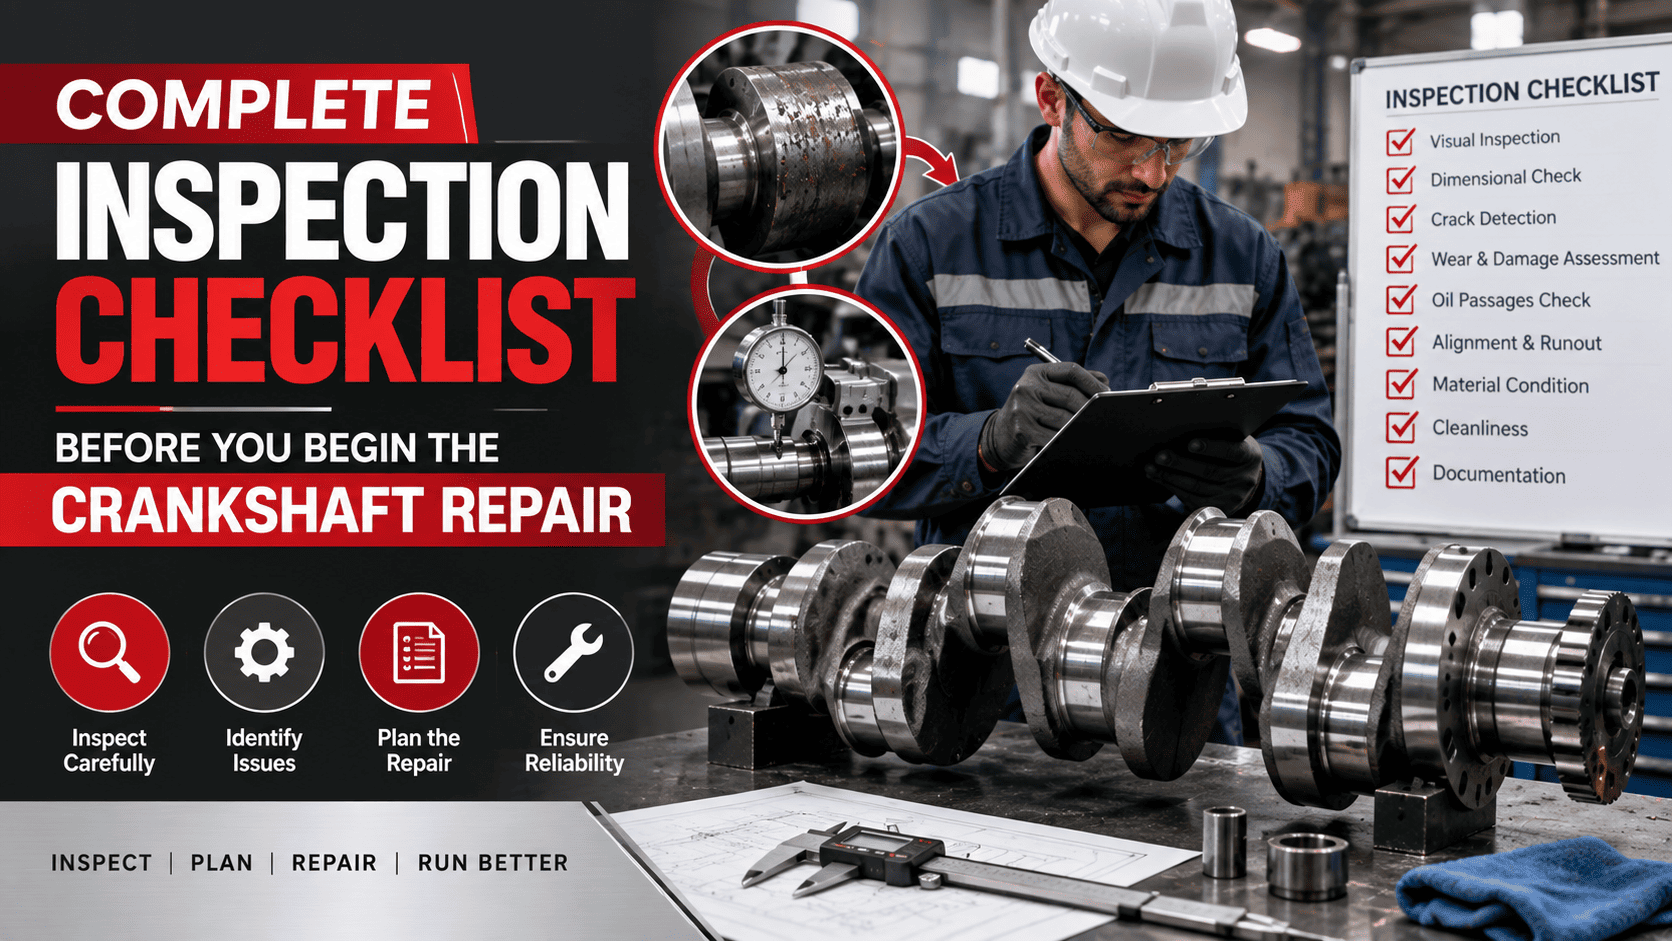
14 Sep Complete Inspection Checklist Before You Begin the Crankshaft Repair
A crankshaft is one of the most important and stressed parts of an engine. In simple words, a crankshaft converts the up and down movement of a piston into rotational motion and generates power.
Notably, crankshafts continuously work under heavy loads. This is why even a small defect sometimes results in
- Unusual vibrations
- Bearing damage
- Oil-pressure problems
- Complete engine failure.
This is the reason why experts begin crankshaft repairing with a deep inspection.
They first look for the actual damage, measure all the critical surfaces, and decide if they can repair the crankshaft safely.
Results? This improves safety, reduces costs, and helps choose the right process.
Why Pre-Repair Inspection Matters?
- Safety
A damaged crankshaft is a big security issue. Even a small structural defect can make the whole crankshaft unsafe. Inspection gives a proper idea of the total current damage.
- Accuracy
Visual inspection cannot tell you all the problems. That’s why technicians use precise tools to measure the damage and check the manufacturer’s specifications.
- Cost Control
Early and regular inspection helps you prevent unnecessary machining. For example, if a journal needs only minor polishing, inspection will help you save the repair costs.
A good inspection answers three important questions:
- What is damaged?
- How severe is the damage?
- What repair method will it need?
Visual Inspection Checklist You Must Look For:
The inspection begins with visual inspection. The technicians clean the crankshaft properly to find the defects.
- Check for Cracks
First, look carefully for cracks. They can be around journals, fillets, keyways, oil holes, and other high-stress areas.
Give more attention to fillets, as changes in them can create stress there.
- Look for Scoring
Look for deep grooves or scoring. They are a sign of poor lubrication, contaminated oil, worn bearings, or foreign particles inside the engine.
Light marks may require polishing, but more serious damage may need grinding.
- Check for Discolouration
Check for discolouration. They generally happen from bearing failure, insufficient lubrication, or excessive friction. Look for blue, purple, or darkened areas as they indicate excessive heat.
Discolouration means changes in the crankshaft’s surface properties, so don’t treat it like a cosmetic issue.
Dimensional Inspection:
After you complete the visual inspection, start measuring the crankshaft accurately.
- Journal Diameter
Use a micrometre and measure every main and connecting rod at multiple points. Compare them to manufacturer’s specifications. The technicians often aim for 0.001 mm accuracy or even better.
Note: don’t assume anything. Check all the journals individually.
- Runout
Runout shows how much a crankshaft journal has shifted from its line. Technicians often use suitable V-Blocks, precise tools, and dial indicators to measure the runout.
Remember to check even the minimum deviation, as it may create high vibration and uneven bearing load. Technicians follow the real manufacturer’s specifications and never rely on the generic number.
- Ovality and Taper
Measure all the journals from different angles and positions. Look for ovality and taper-like conditions. They can cause uneven wear, improper lubrication, misalignment, or prolonged engine operation. Expert technicians measure the journals at 0°, 90°, 180°, and 270°and look for all possible differences.
Surface Condition Assessment:
Next to dimensional measurements, assess the surface for finish and hardness.
- Surface Finish
After you complete the grinding or polishing, your surface should have a proper finish for bearing operation. A rough surface can increase the friction and accelerate bearing wear, whereas an overpolished surface can affect the lubrication. The best technicians use surface-finish measuring equipment.
- Hardness Checks
The crankshaft surface must retain the required hardness to withstand repeated loads and wear.
Excessive grinding, overheating, or previous machining can affect surface hardness. A hardness test can help determine whether the journal remains suitable for repair.
If heat damage is suspected, hardness testing becomes particularly important.
Lubrication and Bearing Inspection:
A crankshaft doesn’t work alone, so you also need to check the connected parts, namely the bearings and the lubrication system.
- Inspect Bearing Wear
Remove the bearings and check them for:
- Uneven wear
- Deep scratches
- Excessive clearance marks
- Copper or base-metal exposure
- Embedded particles
- Signs of overheating
Check for bearing wear patterns, as they also tell about the original cause of crankshaft damage. Look for signs such as:
- Uneven Wear for alignment problems
- Severe Scoring for contaminated oil.
- Inspect Oil Passages
Next, check the Crankshaft oil passages for blockages. Look for the following:
- Dirt
- Sludge
- Carbon deposits
- Metal particles
These small particles can restrict your oil flow.
Note: Clean and inspect every relevant passage before completing the repair.
Advanced Testing Methods:
Remember this: visual and dimensional inspection can’t identify some defects. So, technicians use advanced non-destructive testing to give additional confidence. Here are those:
- Magnetic Particle Testing
Magnetic particle testing, or MPI detects the surface and near-surface cracks in suitable ferromagnetic crankshafts.
For this, technicians first magnetise the component and apply the magnetic particles on its surface. Then they look for disturbances in the magnetic field. This method is especially useful around fillets, keyways, and other high-stress locations.
Ultrasonic Inspection
Ultrasonic testing uses high-frequency sound waves to identify internal discontinuities. It helps you find defects below the surface. Even magnetic particle testing may not reveal this.
Note: the choice of testing method depends on several factors such as:
- Crankshaft material
- Suspected defect
- Equipment available
- Inspection standard
Inspection Report and Repair Planning:
Now, the final step! The expert technicians always end the process with a detailed report. They record and document the following:
- Original journal diameters
- Measured journal diameters
- Runout readings
- Ovality and taper
- Surface condition
- Hardness results
- Crack-testing results
- Bearing condition
- Oil-passage condition
- Recommended repair method
This information creates a clear baseline for the repair. The experts then decide whether the crankshaft needs polishing, grinding, welding and machining, metal spraying, straightening, or replacement.
Note: The repair process of a crankshaft should be based on damage and applicable manufacturer specifications.
Common Mistakes to Avoid During Crankshaft Repair:
- Never skip measurements. Always use tools to identify the damage. A crankshaft can look good and still have excessive taper, ovality, or runout.
- Carefully look for minor defects. Look for small scratches, discoloration, or unusual wear patterns to get the source of damage.
- Before you start the repair, find the root cause of the damage. If the damage is caused by oil starvation, bearing failure, contamination, or misalignment, repairing only the crankshaft won’t be enough.
- Do not use a one-size-fits-all tolerance. Always check the manufacturer’s specifications for references.
Conclusion:
A successful crankshaft repairing process is not just about repairing. Technicians prepare for the procedure properly.
They do a systematic inspection to find issues such as:
- Cracks
- Scoring
- Heat damage
- Dimensional changes
- Surface problems
- Bearing wear
- Lubrication issues.
First, they inspect the crankshaft visually and move to precise measurements and advanced testing. All of these steps reduce the risks and help choose the most economical and technically suitable repair method.
Searching for experts who focus on a systematic approach for crankshaft repair? Connect with MPA Power Project where the technicians follow a pre-set process based on actual component condition, accurate measurements, and proper technical assessment.
No Comments